Maintenance Of Steel Flange
Dec 24, 2019
Maintenance of Steel flange
For workpieces with complex shape or sharp change of cross section and larger effective thickness, preheating should be carried out.
The methods of preheating are: 800?C for one time, 500-550 and 850 for two times. The speed of temperature rise for one time should be limited.
1. Heating:
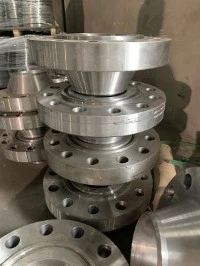
Workpieces, castings and welds with grooves and no through holes, and ASTM A105 CLASS150 Weld Neck Flange,processed and formed, are generally not suitable for heating in salt bath furnaces.
Workpiece heating should have sufficient holding time, depending on the effective thickness and conditional thickness of the workpiece.
2. Cleaning:
Workpieces and fixtures should be cleaned of foreign substances weld neck flange, residual salt and paint before heat treatment.
The fixture used for the first time in vacuum furnace should be degassed and purified in advance at the required vacuum degree of the workpiece.
3. Furnace loading:
Weld neck flange that are easily deformed during heat treatment should be heated on special fixtures.
Work piece should be placed in the effective heating zone.
If you are interested in pipes,fittings and flanges ,please kindly contact below:
Contact person: Ms.Sandy Zhang
Phone/Whats App/Wechat:+86 15127785550
Skype: sandy198607
Email:sandy@yongxingflange.com